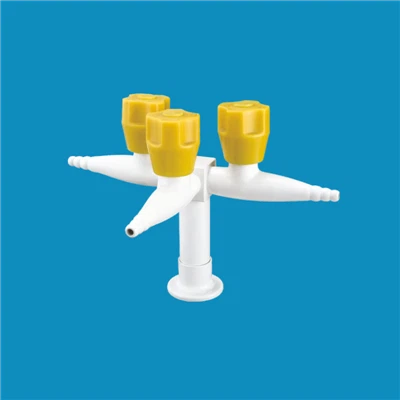
In the modern industrial manufacturing, commercial catering, residential heating, and new energy equipment industries, the safe, stable, and precise control of gas flow has always been the core key to ensuring equipment operation safety, improving energy utilization efficiency, and reducing operational risks. As a professional and high-performance gas control component, the Dual Gas Control Valve has gradually become an indispensable core part of various gas equipment systems relying on its dual-channel independent control structure, ultra-high safety performance, stable adjustment accuracy and wide environmental adaptability. The Dual Gas Control Valve breaks through the structural limitations of traditional single-channel gas control valves, realizes independent and linked dual-path gas supply regulation, and can cope with complex gas supply working conditions that cannot be adapted by ordinary valves. It not only optimizes the overall operating logic of gas equipment but also greatly improves the safety threshold and service life of terminal equipment, making it widely recognized and applied in global industrial and civil gas systems. The Dual Gas Control Valve is professionally designed for medium and high-precision gas supply scenarios such as natural gas, liquefied petroleum gas, and mixed industrial gas, integrating flow regulation, pressure stabilization, safety cut-off and dual-path independent control functions, and is a multifunctional integrated gas control component that integrates safety, efficiency and durability.
With the continuous upgrading of industrial safety production standards and the increasingly stringent civil gas use specifications, the market's requirements for gas control valves are no longer limited to basic gas conduction and cut-off functions, but put forward higher requirements for control accuracy, safety redundancy, structural stability, energy-saving performance and multi-scenario adaptability. Traditional single gas control valves often have obvious functional defects in complex working conditions: single-channel structure cannot support the simultaneous operation of dual burners or dual gas supply circuits, poor pressure stabilization effect leads to unstable gas combustion efficiency, lack of safety redundancy mechanism resulting in high risk of gas leakage in case of component failure, and low adaptability to different gas media and extreme working environments. In contrast, the Dual Gas Control Valve completely solves the above industry pain points through innovative structural design and optimized functional configuration. Its unique dual independent gas circuit design enables two sets of gas supply control systems to operate independently without interfering with each other, and can also realize linkage protection and synchronous regulation according to equipment operating requirements, creating a more reliable and efficient gas supply control solution for all types of gas terminal equipment.
The overall structural design of the Dual Gas Control Valve follows the principles of industrial high strength, standardized assembly and convenient maintenance. The whole valve body adopts integrated die-casting molding process, which avoids the air leakage risk caused by loose assembly gaps of traditional split valve bodies. The internal core components include two groups of independent control spools, high-sensitivity pressure sensing modules, automatic safety cut-off devices, precision flow regulation assemblies and corrosion-resistant sealing structures. Each gas circuit of the Dual Gas Control Valve is equipped with an independent pressure monitoring unit and flow adjusting knob, which can independently adjust the gas flow and output pressure of a single circuit according to the actual operating power of the equipment, realizing precise zoning control of dual gas supply channels. At the same time, the product is equipped with a linkage protection system between dual circuits. When one gas circuit fails in pressure overload, blockage or abnormal flow, the system will automatically trigger the early warning and protection mechanism, which can not only cut off the faulty circuit independently to avoid safety accidents but also ensure the stable operation of the other normal circuit to the greatest extent, avoiding the overall shutdown of the equipment caused by single-point failure, which is an important functional advantage that traditional single gas valves do not have.
In terms of material selection, the Dual Gas Control Valve adheres to high-standard industrial configuration to ensure long-term stable operation in complex working environments. The main valve body is made of high-strength aluminum alloy and stainless steel composite materials. The aluminum alloy main body reduces the overall weight of the product, facilitates equipment assembly and installation, and has excellent compression resistance and impact resistance. The stainless steel lining and core components effectively resist the corrosion of gas media such as sulfide and liquefied petroleum gas, avoiding component aging and failure caused by long-term medium erosion. The internal sealing parts adopt imported high-temperature and oil-resistant rubber materials, which can maintain stable sealing performance in the temperature range of -20℃ to 120℃, and will not produce aging deformation, cracking and air leakage problems due to high-temperature combustion heat radiation or low-temperature environmental freezing. All materials of the Dual Gas Control Valve comply with international CE, UKCA, UL and other industrial safety certification standards, and meet RoHS environmental protection requirements, ensuring that the product has reliable quality and environmental protection performance while realizing functional diversification.
The core advantages of the Dual Gas Control Valve are reflected in multiple dimensions such as functional design, safety performance, control accuracy and service life, and each advantage has been professionally optimized and verified through industrial tests, with extremely prominent practical application value. First of all, the dual-channel independent control advantage of the Dual Gas Control Valve is the core competitive point different from ordinary gas valves. Traditional single gas control valves can only provide a single gas supply output, which can only meet the working requirements of single burner and single gas supply equipment. For dual-burner heating equipment, dual-circuit industrial gas supply systems and multi-power gas equipment, single valves can only realize synchronous opening and closing of the overall gas circuit, unable to adjust the power of a single burner independently, resulting in low equipment operation flexibility and serious energy waste. The Dual Gas Control Valve is equipped with two completely independent gas supply and control circuits inside. Users can adjust the flow rate, pressure and opening degree of each circuit arbitrarily according to the actual operating demand of the equipment. For example, in commercial double-head cooking stoves, the two gas circuits of the Dual Gas Control Valve can correspond to the two stove heads respectively. When a single stove head is used alone, the corresponding single gas circuit can be opened independently, and the other circuit remains closed and sealed, avoiding unnecessary gas loss; when double stove heads work at the same time, the two circuits can adjust different gas output powers according to different cooking heat requirements, realizing precise matching of heat energy and processing requirements, and greatly improving the flexibility and energy-saving effect of equipment operation.
Secondly, the Dual Gas Control Valve has industry-leading high-precision pressure stabilization and flow regulation performance, which effectively solves the common problem of unstable gas combustion in traditional gas equipment. In the actual gas supply process, affected by pipeline gas pressure fluctuation, pipeline blockage, gas medium purity and other factors, the gas output pressure of ordinary valves often fluctuates greatly, leading to unstable combustion flame, insufficient combustion, excessive gas consumption, and even equipment flameout and tempering phenomena, which not only reduces equipment work efficiency but also brings potential safety hazards. The Dual Gas Control Valve is built-in with a high-precision pressure sensing and self-stabilizing system. Each independent gas circuit is equipped with a micro-pressure regulator, which can monitor the real-time pressure of the gas circuit in real time with a monitoring accuracy of up to ±0.1kPa. When the pipeline gas pressure fluctuates suddenly, the internal regulating spool of the Dual Gas Control Valve can respond in milliseconds, automatically adjust the opening of the valve port, dynamically balance the input and output gas pressure, and keep the output gas pressure and flow rate in a constant stable state. This precise regulation performance ensures that the gas can be fully and uniformly burned in the combustion equipment, effectively improving gas combustion efficiency, reducing gas waste, and avoiding incomplete combustion resulting in carbon monoxide excess and environmental pollution. In industrial heating furnaces and constant-temperature heating equipment, this stable control performance can also ensure the stability of equipment temperature control, improve product processing qualification rate, and reduce production loss caused by temperature fluctuation.
Thirdly, the Dual Gas Control Valve has a multi-layer safety protection mechanism, which comprehensively improves the safety level of gas equipment operation and eliminates potential safety hazards in the whole working process. Safety is the primary evaluation index of gas control components, and traditional gas valves usually only have basic manual cut-off and simple overpressure protection functions, with single protection means and poor fault tolerance. Once the internal valve core is stuck, the pressure sensor fails or the pipeline leaks, it is easy to cause gas leakage, deflagration and other serious safety accidents. The Dual Gas Control Valve has built-in multiple safety protection functions such as overpressure automatic cut-off, underpressure protection, flameout protection, leakage self-detection and over-temperature protection, forming a full-cycle safety protection system. When the gas circuit pressure exceeds the set safe threshold, the overpressure protection module of the Dual Gas Control Valve will automatically close the valve port of the corresponding circuit within 0.5 seconds to prevent high-pressure gas from impacting the equipment and causing pipeline rupture and gas leakage; when the pipeline pressure is too low to support normal combustion, the underpressure protection device will automatically cut off the gas supply to avoid unstable combustion and tempering accidents caused by insufficient gas pressure; when the equipment suddenly goes out during operation, the flameout sensing module will quickly trigger the cut-off mechanism to prevent a large amount of unburned gas from accumulating in the equipment and causing deflagration risks. In addition, the Dual Gas Control Valve is also equipped with a physical anti-leakage sealing structure. Even if the equipment is in a long-term standby state, the internal double-layer sealing design can effectively prevent micro-leakage of gas, ensuring the safety of equipment standby and use.
Fourthly, the Dual Gas Control Valve has excellent durability and environmental adaptability, and can maintain long-term stable operation in various harsh working environments. Most ordinary gas control valves on the market have low environmental adaptability, and are prone to failure problems such as valve core jamming, sealing aging and pressure regulation failure in high-temperature, low-temperature, humid and dusty environments, resulting in short service life of the product and frequent maintenance and replacement, which increases the operating cost of equipment. The Dual Gas Control Valve has undergone professional anti-corrosion, anti-high temperature, anti-low temperature and anti-dust treatment in the overall design. The internal precision components are encapsulated with dust-proof and moisture-proof layers, which can effectively isolate the interference of external dust, water vapor and corrosive media. The valve core adopts a polished precision process, with smooth surface and no friction dead angle, which can avoid jamming failure caused by long-term friction and gas impurity deposition. After industrial durability tests, the continuous working life of the Dual Gas Control Valve can reach more than 80,000 hours, which is far higher than the 30,000-40,000 hours service life of ordinary single gas valves. It can adapt to long-term uninterrupted operation of industrial equipment and frequent start-stop operation of civil equipment, greatly reducing the frequency of product maintenance and replacement, and saving a lot of later operation and maintenance costs for users.
Fifthly, the Dual Gas Control Valve has the advantages of simple installation and convenient maintenance, which can effectively reduce the assembly cost and later maintenance difficulty of equipment manufacturers. The product adopts a standardized modular integrated design, with unified interface specifications, which is compatible with most mainstream gas equipment pipelines on the market. Users do not need to modify the equipment pipeline structure during installation, and can realize quick assembly and docking through standard thread interfaces and flange interfaces. The overall structure of the Dual Gas Control Valve is compact and reasonable, with a small overall volume, which does not occupy the internal space of the equipment, and is convenient for the structural layout of miniaturized and integrated gas equipment. In terms of maintenance, the modular split structure of the Dual Gas Control Valve enables each functional module to be disassembled and replaced independently. When a single gas circuit or a single functional component fails, users only need to replace the corresponding faulty module without disassembling the whole valve body, which greatly simplifies the maintenance process, shortens the maintenance time, and improves the operating efficiency of the equipment. Compared with the integrated non-detachable structure of traditional gas valves, this modular design greatly reduces the maintenance cost and improves the product's after-sales service convenience.
In terms of application scenarios, the Dual Gas Control Valve has extremely wide versatility, covering civil commercial, industrial production, special equipment and other multi-field gas supply control scenarios, and can realize targeted functional adaptation according to different working condition requirements. In the commercial catering industry, the Dual Gas Control Valve is widely used in commercial double-head gas stoves, multi-head cooking equipment, commercial soup stoves, steaming stoves and large kitchen gas equipment. Commercial kitchen equipment usually needs to cope with diversified cooking demands such as high-fire stir-frying, low-fire simmering and constant-temperature steaming. The dual independent control function of the Dual Gas Control Valve can perfectly match the differentiated heat demand of double-stove equipment. Catering merchants can adjust the gas output of the two circuits independently according to different cooking processes, which not only ensures the cooking effect of dishes but also avoids gas waste caused by single-power simultaneous gas supply of double stoves. At the same time, the multi-layer safety protection mechanism of the Dual Gas Control Valve can effectively avoid gas leakage and flameout deflagration accidents in dense catering environments, ensuring the safety of commercial kitchen operation.
In the field of industrial production and heating, the Dual Gas Control Valve is applied to industrial gas heating furnaces, constant-temperature drying equipment, gas heat treatment furnaces, industrial boiler auxiliary gas supply systems and chemical gas reaction equipment. Industrial gas equipment has high requirements for gas supply stability and control accuracy. Slight gas pressure fluctuation will lead to unqualified product processing and affect production quality. The high-precision self-stabilizing regulation performance of the Dual Gas Control Valve can maintain long-term constant gas supply pressure and flow, ensure the stable combustion state of industrial furnaces, and provide stable heat support for industrial processing. For dual-cavity industrial heating equipment and multi-stage heating systems, the dual-channel linkage control function of the Dual Gas Control Valve can realize staged gas supply and power adjustment, meet the heating requirements of different processing stages, and greatly improve the intelligence and refinement level of industrial production. In addition, the excellent high-temperature resistance and corrosion resistance of the Dual Gas Control Valve enable it to adapt to high-temperature and high-dust industrial working environments, avoiding frequent equipment failures caused by harsh working conditions and ensuring the continuity of industrial production.
In the field of civil heating and household gas equipment, the Dual Gas Control Valve is suitable for dual-circuit wall-mounted gas boilers, household dual-head gas stoves, gas water heaters with dual heating channels and indoor gas heating equipment. With the continuous improvement of household living standards, household gas equipment is developing towards multi-function and high-efficiency. Traditional single-channel gas valves cannot meet the needs of multi-functional household gas equipment. The Dual Gas Control Valve can realize independent control of dual heating channels of household boilers, realize the separate operation of domestic hot water supply and indoor heating, and avoid mutual interference between the two functional systems. When users only need domestic hot water, they can start the single gas circuit for hot water heating; when indoor heating is needed at the same time, they can start the dual gas circuit for synchronous operation, which flexibly meets the diversified living needs of families and effectively reduces household gas consumption. At the same time, the ultra-high safety performance of the Dual Gas Control Valve provides a strong safety guarantee for household gas use, effectively avoiding household gas safety accidents caused by equipment failure.
In the field of special equipment and new energy equipment, the Dual Gas Control Valve is also widely used in RV gas equipment, outdoor mobile gas devices, agricultural drying and heating equipment, hydrogen mixed gas supply systems and low-power industrial gas power equipment. These special equipment scenarios have high requirements for product volume, stability and environmental adaptability. The compact structure and strong environmental adaptability of the Dual Gas Control Valve can adapt to mobile working conditions and extreme temperature environments. For agricultural drying equipment that needs long-term outdoor operation, the dust-proof and anti-corrosion performance of the Dual Gas Control Valve can resist outdoor wind and rain erosion and dust deposition, ensuring stable operation of the equipment throughout the year; for new energy hydrogen-mixed gas equipment, the precise flow regulation performance of the Dual Gas Control Valve can realize the proportional mixing and stable supply of mixed gas, meeting the technical requirements of new energy gas combustion.
In order to more intuitively reflect the product advantages of the Dual Gas Control Valve, it is necessary to conduct in-depth comparative analysis with traditional single gas control valves and ordinary double gas valves on the market. First of all, compared with traditional single gas control valves, the Dual Gas Control Valve has a qualitative leap in functional diversity and application scope. Traditional single gas valves only have a single gas supply channel, which can only support single-point gas supply and single-power operation, and cannot adapt to dual-burner and multi-functional gas equipment. In terms of safety performance, single gas valves only have basic overpressure protection, lacking flameout protection, underpressure protection and dual-circuit linkage protection functions, with low safety redundancy and high operational risk. In terms of regulation accuracy, the pressure regulation error of single gas valves is generally ±0.5kPa, which is easy to cause unstable combustion and low energy utilization efficiency. In contrast, the Dual Gas Control Valve adopts dual independent circuit design, supports multi-mode operation of single-circuit independent work and dual-circuit synchronous work, and covers almost all civil and industrial gas supply scenarios. Its multi-dimensional safety protection system realizes full coverage of fault early warning and protection, and the pressure regulation accuracy is increased to ±0.1kPa, which greatly improves gas combustion efficiency and equipment operation stability. Although the purchase cost of the Dual Gas Control Valve is slightly higher than that of single gas valves, its long service life, low maintenance cost and high energy-saving benefit can help users save a lot of comprehensive operating costs in the later stage, with higher overall cost performance.
Secondly, compared with ordinary double gas valves on the market, the Dual Gas Control Valve has obvious advantages in structural design and functional optimization. Most ordinary double gas valves adopt semi-independent dual-circuit design, the internal two gas circuits are linked in structure, and the pressure regulation and flow control are synchronous, which cannot realize independent adjustment of a single circuit, essentially belonging to the expanded version of single gas valves, and cannot solve the problem of differentiated power regulation of dual equipment. In terms of safety structure, ordinary double gas valves have a single protection mechanism. When one circuit fails, it is easy to cause the overall failure of the valve body, resulting in equipment shutdown and gas leakage risks. In terms of material technology, most ordinary double gas valves adopt ordinary cast iron and ordinary rubber sealing materials, which have poor corrosion resistance and high temperature resistance, and are prone to aging and failure after long-term use. The Dual Gas Control Valve adopts a fully independent dual-circuit isolation structure, with completely independent gas transmission, regulation and protection systems for the two circuits, zero mutual interference, and truly realizing independent control of dual channels. In terms of safety protection, the dual-circuit independent protection mechanism of the Dual Gas Control Valve can realize single-circuit fault isolation, ensuring that the faulty circuit is safely cut off and the normal circuit operates stably, which greatly improves the fault tolerance of the equipment. In terms of materials and technology, the high-strength composite materials and precision processing technology adopted by the Dual Gas Control Valve make its overall performance far superior to ordinary double gas valves, with longer service life and more stable long-term operation performance.
In terms of energy-saving and environmental protection performance, the advantages of the Dual Gas Control Valve are also very prominent. Traditional gas control valves have low regulation accuracy, resulting in excessive gas supply in the actual working process, incomplete combustion and serious gas waste, and the unburned gas will also produce harmful gases such as carbon monoxide, causing environmental pollution. The precise flow and pressure regulation function of the Dual Gas Control Valve can accurately match the gas supply volume according to the actual heat demand of the equipment, realizing quantitative gas supply and full combustion, effectively improving gas utilization efficiency by 15%-25% compared with ordinary valves, greatly reducing gas consumption and operating costs. At the same time, the full combustion of gas reduces the emission of harmful combustion products, which is more in line with modern industrial energy-saving and environmental protection production standards and civil low-carbon use requirements. For enterprises and users who pursue energy-saving consumption reduction and green production, the Dual Gas Control Valve is an ideal high-efficiency and energy-saving gas control component.
In terms of product certification and quality assurance, all batches of the Dual Gas Control Valve have passed strict industrial performance tests and international authoritative safety certifications, including CE European safety certification, UKCA British market certification, UL American industry certification and RoHS environmental protection certification. Each product will undergo strict factory tests such as air tightness test, pressure resistance test, flow regulation accuracy test and high and low temperature cycle test to ensure that every Dual Gas Control Valve leaving the factory meets high-standard industrial quality requirements. In the actual market application process, the Dual Gas Control Valve has withstood the test of various complex working conditions, and has stable product quality and low failure rate, winning high recognition from equipment manufacturers, engineering contractors and terminal users at home and abroad.
In terms of product scalability and matching performance, the Dual Gas Control Valve supports personalized functional customization and multi-specification matching, which can meet the differentiated needs of different industries and different equipment power levels. The product has formed a complete specification system from small-flow civil type to large-flow industrial type, which can accurately match household small gas equipment, commercial medium-power equipment and industrial high-power gas supply systems. At the same time, the Dual Gas Control Valve can be matched with intelligent control modules, temperature sensing modules and remote monitoring modules to realize intelligent automatic control such as remote gas supply switching, automatic power adjustment and fault remote early warning, which is compatible with the intelligent upgrading trend of modern gas equipment and has strong product scalability and market adaptability.
In conclusion, the Dual Gas Control Valve, with its unique dual independent control structure, ultra-high safety performance, precise regulation ability, excellent environmental adaptability and diversified scenario matching advantages, has become an upgraded alternative to traditional gas control valve products. The Dual Gas Control Valve not only solves many functional defects and safety hidden dangers of traditional gas valves in practical application but also realizes the integration of high efficiency, energy saving, safety and intelligence of gas supply control, which can effectively improve the operating efficiency of gas equipment, reduce the operating cost of equipment, and ensure the safety and stability of gas use. With the continuous development of the gas equipment industry towards high efficiency, safety and intelligence, the Dual Gas Control Valve will be more widely used in various civil, commercial and industrial fields, and become a core basic component to promote the overall upgrading of the gas control industry. Whether it is for equipment manufacturers to improve product competitiveness, or for terminal users to reduce use risks and save energy costs, the Dual Gas Control Valve can provide high-value professional solutions, and has extremely high market application value and industry development prospects.
Features
Refined copper material: Corrosion-resistant, high-temperature-resistant, and effective in preventing rust.
Epoxy resin spray painting: high-temperature resistant baking paint process, combining practicality with aesthetics


Product Specification
|
Main Body |
Thickened copper material |
|
Coating |
High-brightness epoxy resin coating, corrosion-resistant, heat-resistant, and UV radiation-proof |
|
Valve Core |
High-precision ceramic snap valve core, standard safety type valve core, with a switch life of up to 550,000 times, static pressure resistance of 40 bars |
|
Accessory |
Detachable brass serrated nozzle,splash-controlled water filter attachable |
|
Switch knob |
ABS knob, elegant, generous, ergonomic design, lightweight, durable |
|
Outlet |
Reduce the water outlet and install a spray splash faucet |
|
Advantage |
Long-lasting and durable |


Application

Services
1. Product quality control and delivery time is strictly controlled;
2. Direct manufacturing factory offering competitive price;
3. All the inquiries will be replied within 12 hours;
4. OEM & ODM service are available;
5. Providing first-class after-sales services to the customers.
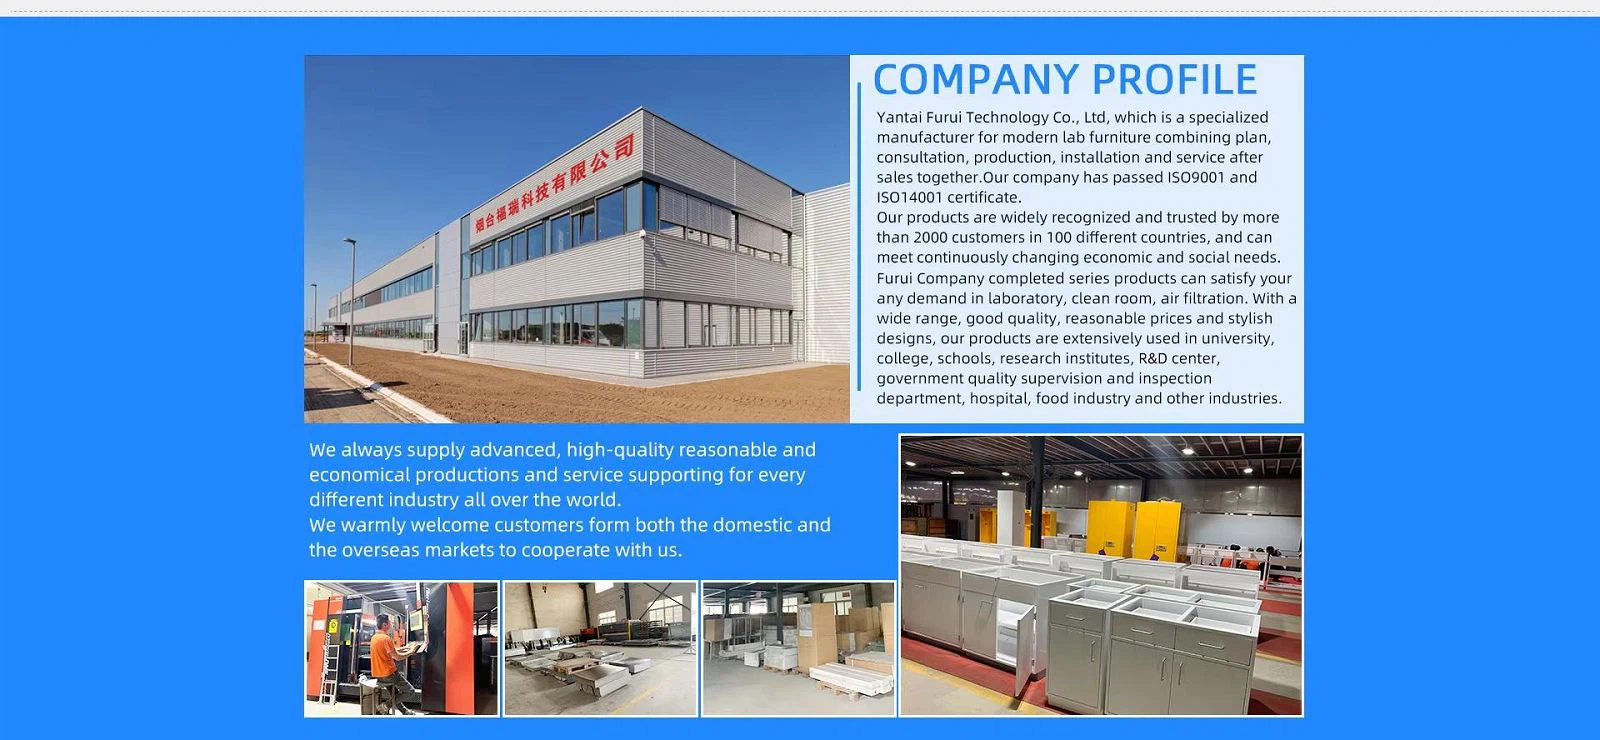

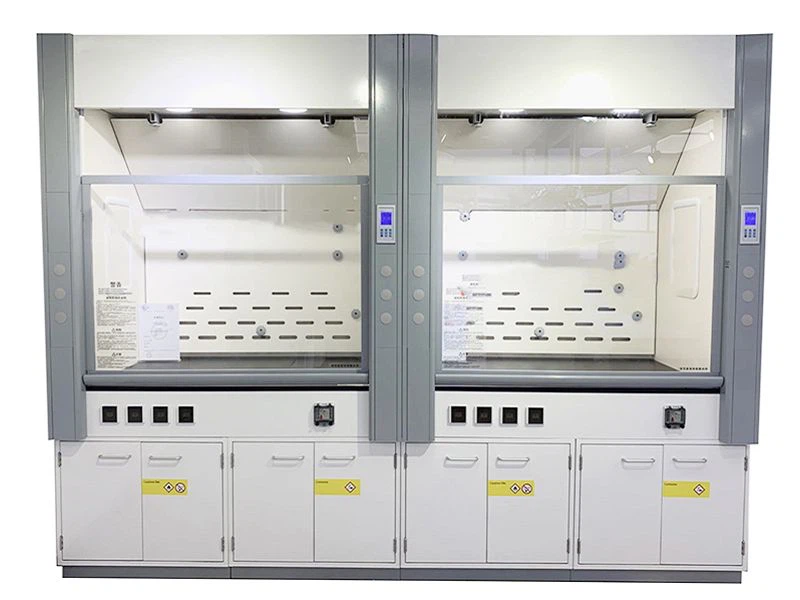
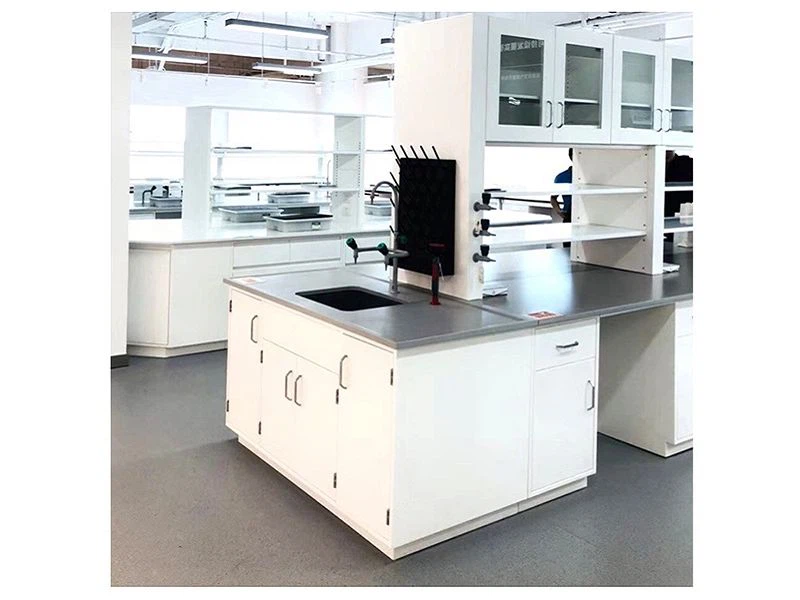
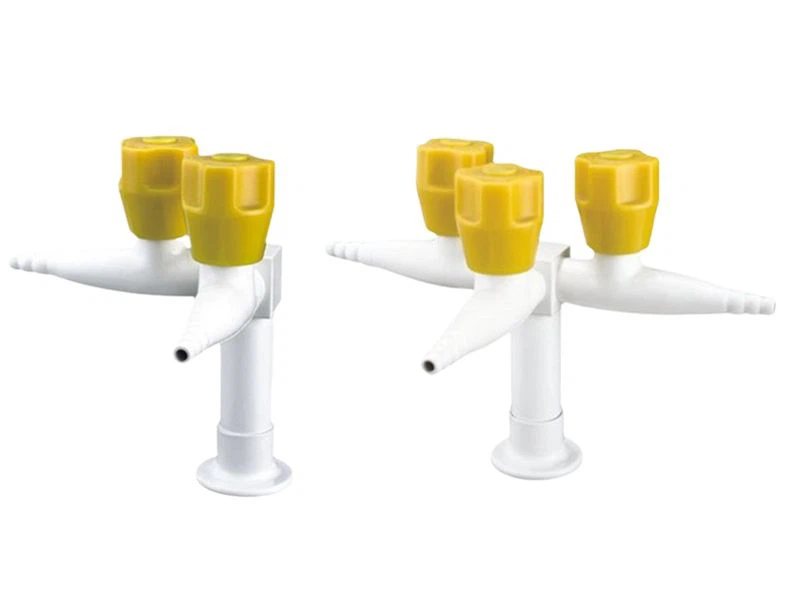
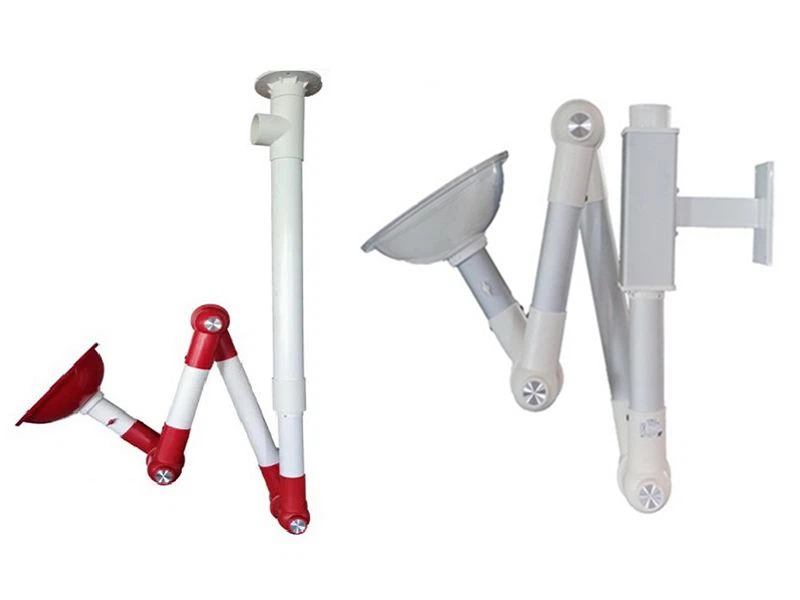
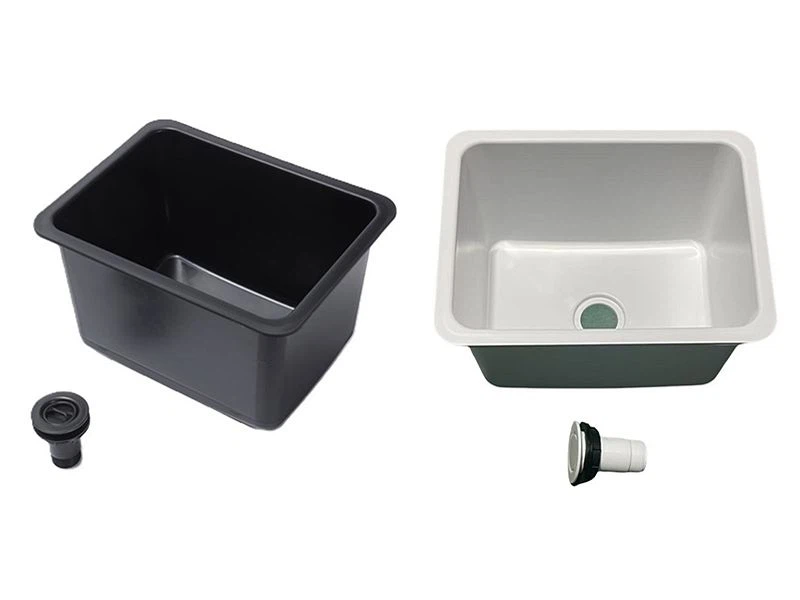
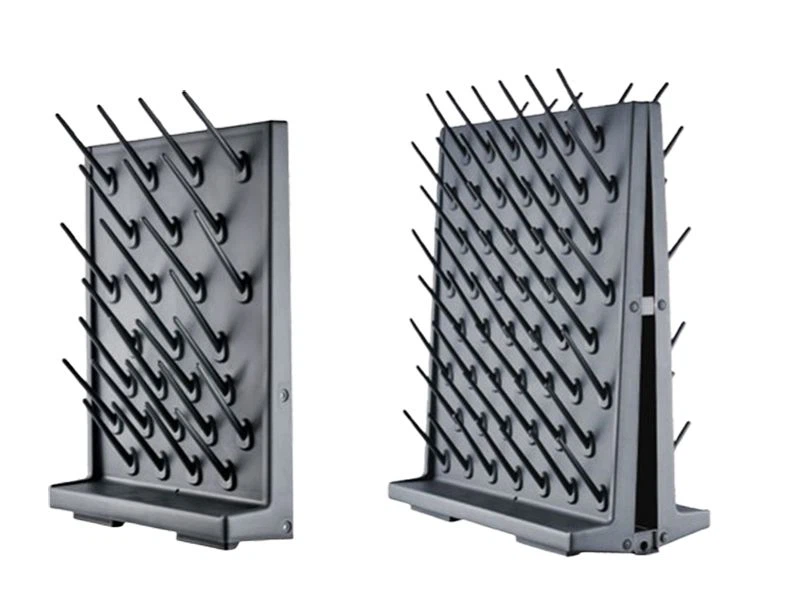
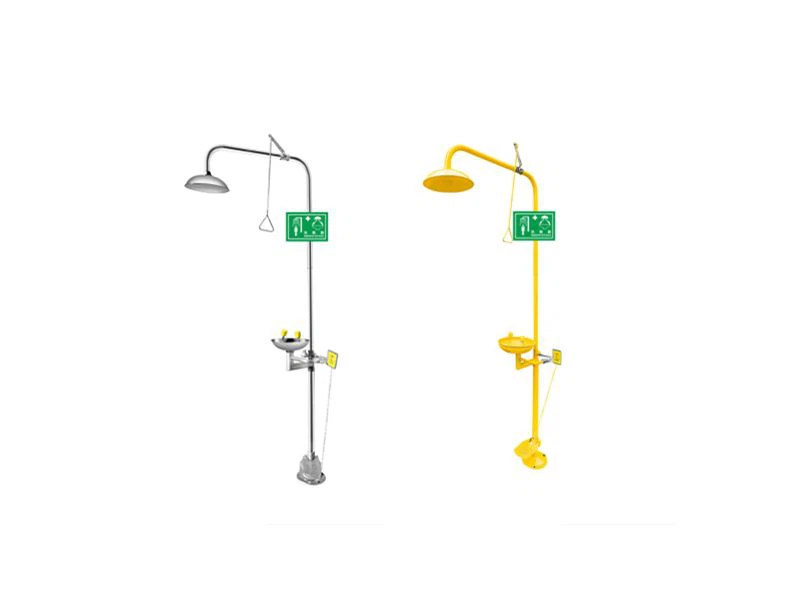
We are in Yantai, China. Our main productions include Lab Furniture, Fume Hood,Workbench,Lab cabinet etc; Lab Accessories, Faucet, Fume Extaction Arm, Lab Pegboard, Lab Chair, Lab Gas Tap, PP Sink, Eye Wash etc. Up to now, Our products have been exported to more than 30 countries, such as Russia, Kuwait, Mexico, Malaysia, Kazakhstan, India, Philippines, South Korea, South Africa, Indonesia, Thailand etc. So we can provide high service to our clients.
Main Products
FAQ
Q: How can I place an order?
A: You can contact any of our sales person for an order. Please provide the details of your requirements as clear as possible. So we can send you the offer at the first time.
For designing or further discussion, it is better to contact us with Skype, TradeManger or QQ or WhatsApp or other instant ways, in case of any delays.
Q: When can I get the price?
A: Usually we quote within 24 hours after we get your inquiry.
Q: What about the lead time for mass production?
A: Honestly, it depends on the order quantity and the season you place the order.
Alway 25-28days based on general order .
Q: What is your terms of delivery?
A: We accept EXW, FOB, CFR, CIF, etc. You can choose the one which is the most convenient or cost effective for you.
Q: What is the payment way?
A: 1)TT or Wester Union for the trial order
2)ODM, OEM order, 30% for deposit,70% against the copy B/L.
Hot Tags: dual gas control valve, China dual gas control valve manufacturers, suppliers, factory, Double Gas Tap, Four Gas Tap, lab accessories, lab gas tap, Single Gas Tap, Three Gas Tap